
HGYS150-V4-EV Full-Servo ISBM Machine — Alternative to NISSEI ASB-12M
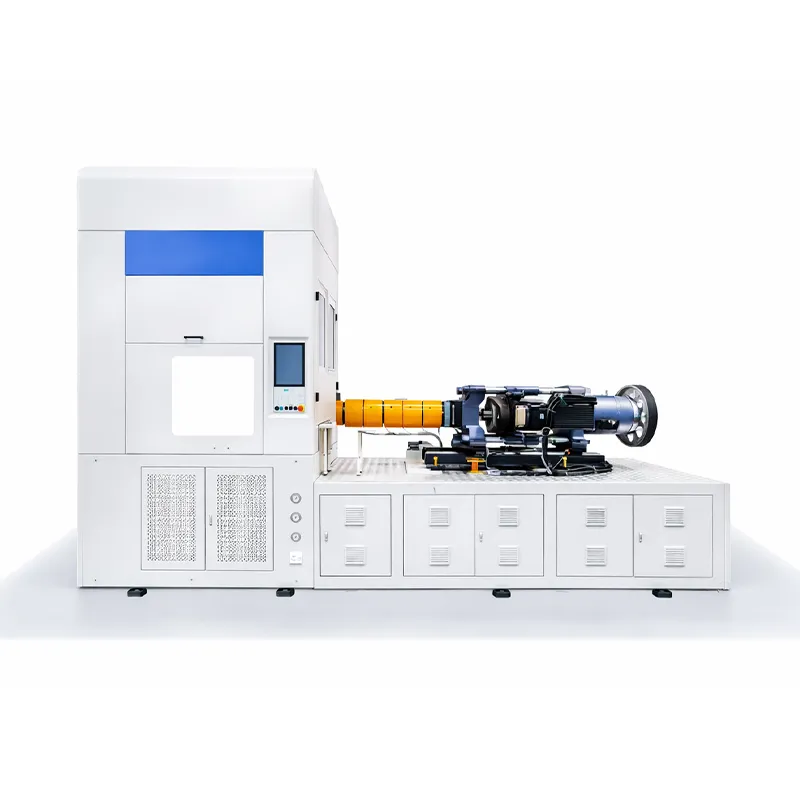
Ten independent servo motors. 350 rpm across every screw size. 392 g shot capacity at ø50 mm — 26% more than the standard HGY150-V4. The Korea Ever-Power HGYS150-V4-EV is the full-servo version of our ASB-12M class ISBM machine, built for production lines where wall-thickness tolerance, cycle speed, and output volume are all non-negotiable at the same time. NISSEI ASB-12M mould tooling mounts directly — no re-tooling cost, no qualification delay. Shot-weight repeatability under 0.3% per cycle. Nano far-infrared heated barrel, NSK Japan lead screws, Parker USA valves standard. Footprint 5,200 × 1,800 × 3,300 mm, 7 T. PET and PETG, 20 ml to 2,500 ml, up to 8 cavities.
Why Full-Servo Changes the Output Equation
Most machines at the ASB-12M capacity level share a hydraulic or servo-pump architecture — meaning one pressure circuit feeds multiple axes, and every axis competes for flow. The Korea Ever-Power HGYS150-V4-EV replaces that shared circuit with 10 independent servo motors, each controlling a single axis in closed-loop. The injection unit, clamping, turntable, take-out, and conditioning station each run on their own servo with their own feedback — which is why this machine holds shot-weight variation below 0.3% per cycle where a pump-servo machine typically drifts to 0.8–1.5% on thin-wall formats.
The productivity numbers follow. Screw rotational speed is 350 rpm uniform across all screw diameter options — ø40, ø50, and ø55 mm all run at 350 rpm, versus 270 / 180 / 150 rpm respectively on the standard HGY150-V4. The standard ø50 mm screw delivers 392 g injection capacity, 26% above the HGY150-V4's 310 g at the same screw size.
And the mould situation is straightforward: NISSEI ASB-12M tooling mounts directly — same platen geometry, no adapter plates, no re-qualification. Factories with existing ASB-12M mould sets switch to the HGYS150-V4-EV and start production on day one with their validated tooling.
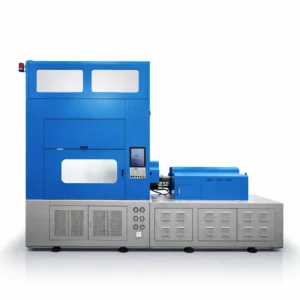
HGYS150-V4-EV — 4-Station Full-Servo One-Step ISBM Machine
Technical Specifications
| Parameter | Value |
|---|---|
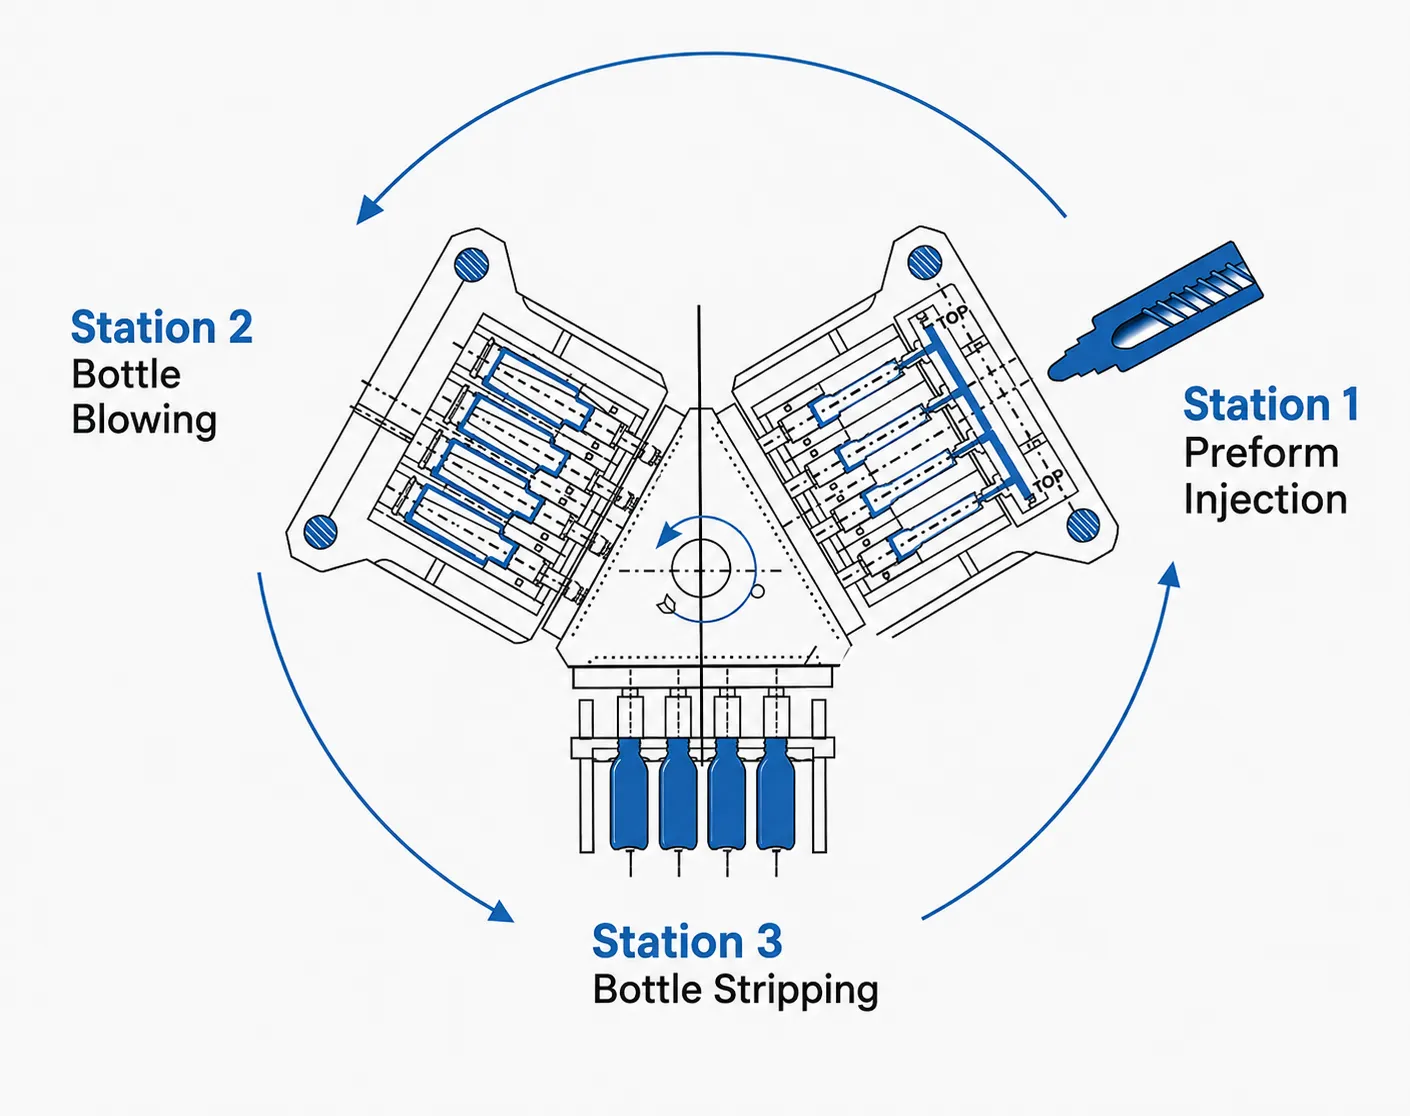
| Machine Layout | 4-station rotary — Injection / Conditioning / Stretch Blow / Take-out |
| Drive System | 10 sets full servo motor control (Inovance / WEICHI) — 102.8 KW |
| Screw Diameter | ø40 / ø50 / ø55 mm |
| Theoretical Injection Volume | 188 cm³ (ø40) / 392 cm³ (ø50) / 475 cm³ (ø55) |
| Shot Capacity (ø50 standard) | 392 g (+26% vs HGY150-V4 at same screw diameter) |
| Screw Rotational Speed | 350 rpm — uniform across all screw diameter options |
| Injection Clamping Force | 150 KN |
| Blowing Clamping Force | 200 KN (single side) — dual servo motor clamping with high-pressure compensation |
| Heating | 10 KW nano far-infrared energy-saving heating ring |
| Total Installed Power | 112.8 KW |
| Lead Screw | NSK Japan |
| Key Components | Parker valves (USA) · NSK lead screws (Japan) · Yaskawa / WEICHI servo turntable · Airtak cylinders |
| Blowing Air Pressure | 2.0 – 3.5 MPa |
| Cooling Water Pressure | 0.4 – 0.6 MPa |
| Voltage | 370 – 400 V |
| Machine Dimensions (L × W × H) | 5,200 × 1,800 × 3,300 mm |
| Machine Weight | 7 T |
| Compatible Materials | PET, PETG |
| ASB-12M Mold Fit | Compatible — direct mount, no modification required |
| Certification | CE + ISO 9001:2015 |
Bottle Cavity Matrix — HGYS150-V4-EV
| Cavities | Body Ø (mm) | Max Height (mm) | Neck Ø (mm) | Max Volume (ml) | Max Weight (g) |
|---|---|---|---|---|---|
| 1 | 118 | 210 | 83 | 2,500 | 130 |
| 2 | 80 | 210 | 62 | 1,500 | 65 |
| 3 | 66 | 150 | 48 | 900 | 43 |
| 4 | 56 | 150 | 38 | 400 | 32 |
| 5 | 54 | 150 | 32 | 250 | 26 |
| 6 | 45 | 150 | 25 | 100 | 22 |
| 7 | 28 | 100 | 17 | 30 | 18 |
| 8 | 26 | 100 | 15 | 20 | 16 |
HGYS150-V4-EV vs NISSEI ASB-12M — Head-to-Head
Where ASB-12M technical data is not published, values are noted as N/A. Korea Ever-Power recommends buyers request complete ASB-12M specifications directly from Nissei ASB Machine Co., Ltd. for a full numerical evaluation.
| Parameter | Korea Ever-Power HGYS150-V4-EV | NISSEI ASB-12M (Reference) |
|---|---|---|
| Drive Architecture | 10 independent servo motors — full closed-loop per axis | Servo-driven (proprietary) |
| Max Injection Capacity | 392 g (ø50 mm) higher output ceiling | N/A (not published) |
| Screw Rotational Speed | 350 rpm — uniform all screw sizes fastest in class | N/A (not published) |
| Shot-Weight Repeatability | < 0.3% per cycle | N/A (not published) |
| Inj. Clamping Force | 150 KN | N/A (not published) |
| Mold Interchangeability | ASB-12M direct mount — no re-tooling cost | OEM tooling only |
| Total Installed Power | 112.8 KW | N/A (not published) |
| Machine Dimensions | 5,200 × 1,800 × 3,300 mm / 7 T | N/A (not published) |
| Delivery Lead Time | 45 – 75 days | 12 – 18 months (new machine) |
| Spare Parts | Open-market (Parker, NSK, Yaskawa) | OEM-only |
| On-Site Commissioning | Included (Korea, SEA) | At extra cost |
| Certification | CE + ISO 9001:2015 | CE |
Three Advantages That Separate HGYS150-V4-EV From the ASB-12M Class
Where HGYS150-V4-EV Outperforms
Pharmaceutical Dropper Vials and Precision Closure Containers
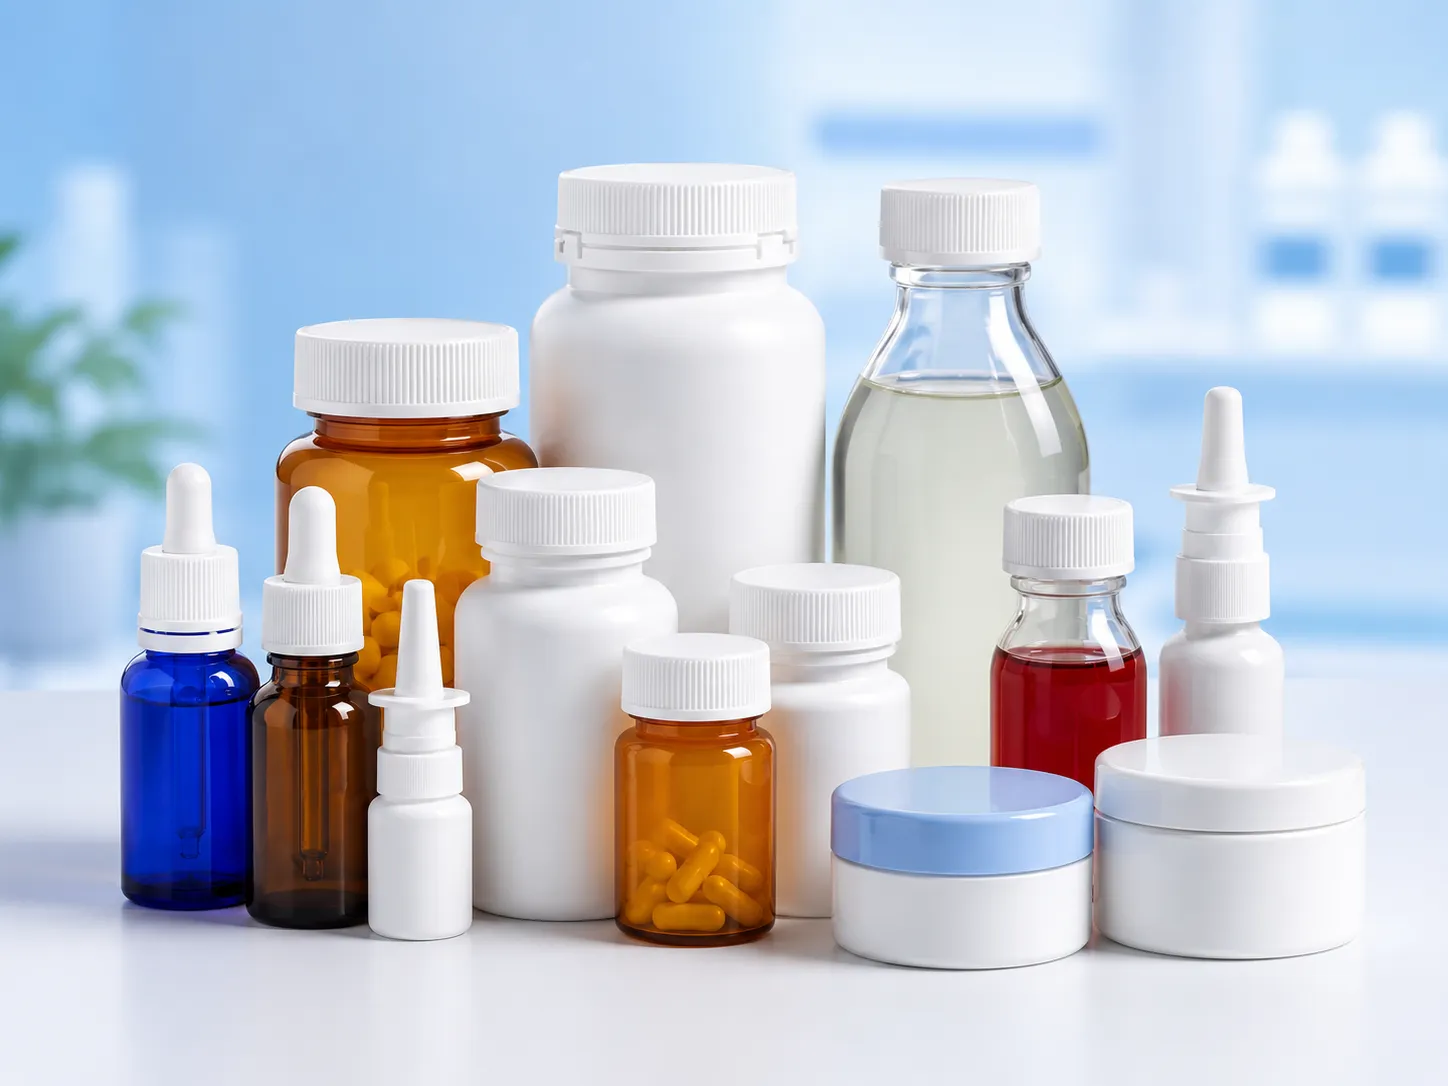
This is the application class where <0.3% shot-weight repeatability is not a marketing claim but a fill-line operational requirement. Eyedrop bottles, oral liquid vials, and dropper containers with precision neck finishes live or die on wall-thickness consistency at the neck — the parameter that determines closure torque and leak rejection rate on pharmaceutical filling lines. The HGYS150-V4-EV's full-servo closed-loop injection maintains this tolerance across all cavity positions throughout a full production shift, without the drift that pump-servo machines accumulate as hydraulic fluid warms. 4 to 8 cavities, 20 ml to 400 ml. Regulatory documentation available on request.
Luxury Cosmetic and K-Beauty — Thin-Wall PETG Serum Bottles
Thin-wall PETG serum and essence containers for premium cosmetic brands sit at the intersection of maximum clarity and minimum material usage — a combination that punishes any shot-weight variation with visible thickness bands in the bottle body under retail lighting. The HGYS150-V4-EV's ten independent servo axes hold wall distribution consistent across all 8 cavity positions per cycle. The nano far-infrared barrel prevents the localised temperature hot-spots that cause clarity variation in PETG at sustained production rates. 3 to 6 cavities, 30 ml to 250 ml, ASB-12M tooling.
Baby Care — BPA-Free Feeding Bottles
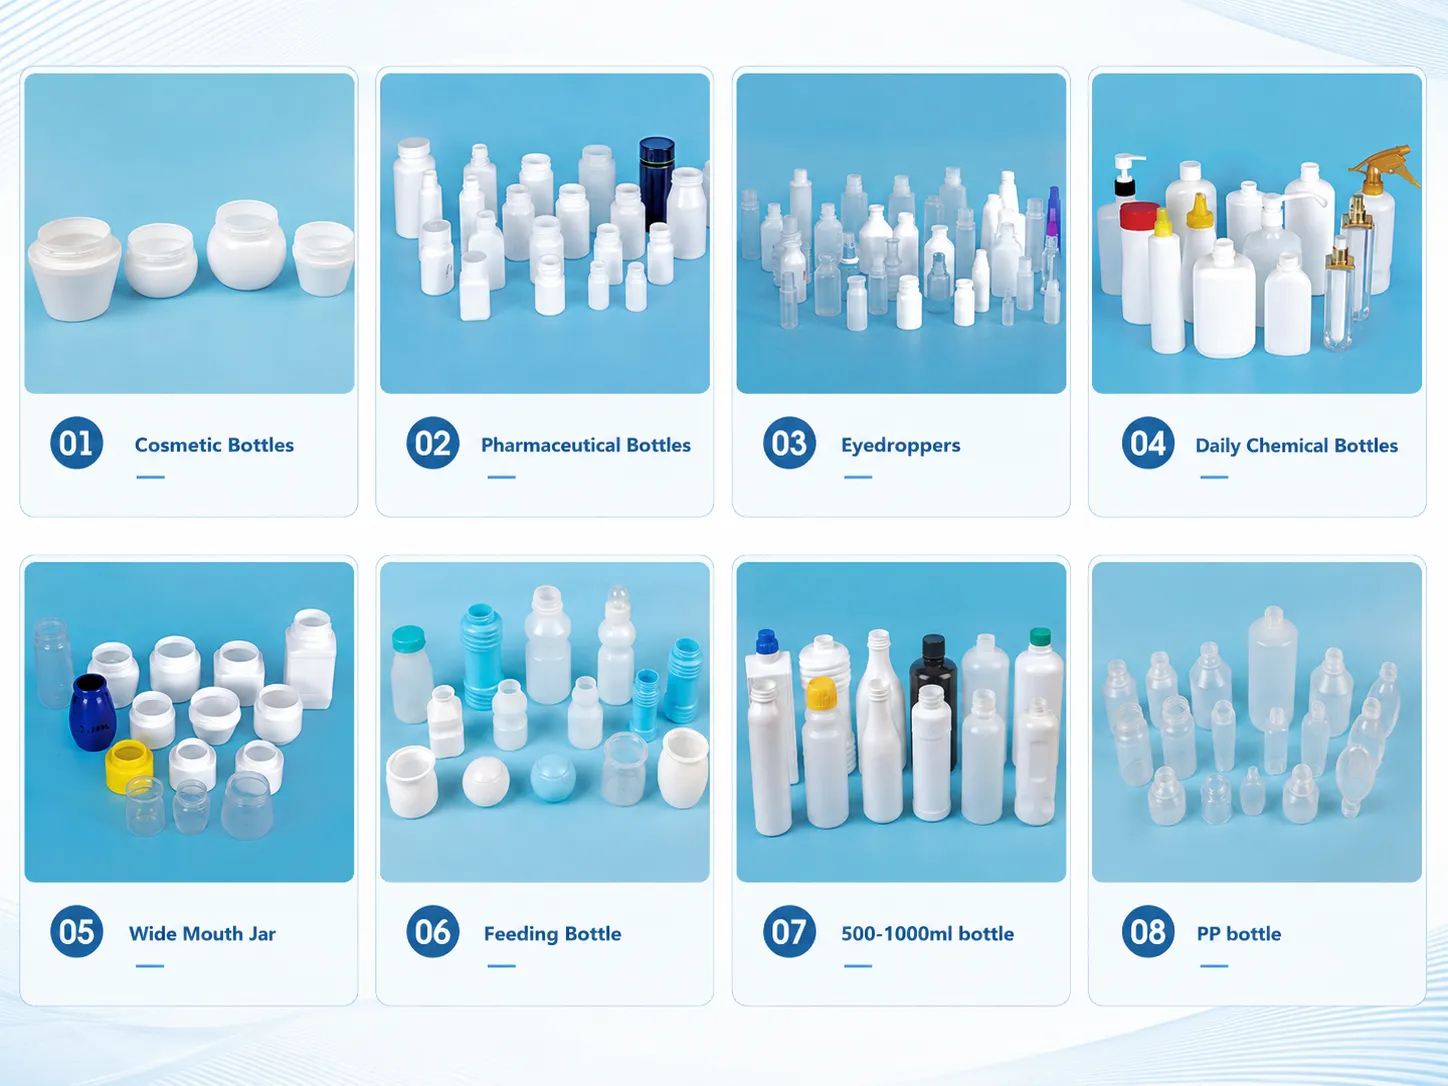
PETG baby feeding bottles and infant oral medicine containers where material purity, neck-finish precision, and visual wall clarity are brand requirements. Full-servo drive and nano far-infrared barrel maintain PETG clarity and mechanical consistency at sustained production rates. 1 to 3 cavities, 100–250 ml.
High-Volume Small Format — Maximum Output on Existing Moulds
Where the goal is maximum bottles per shift from an existing ASB-12M mould set, 350 rpm uniform screw speed directly shortens cycle time across all 8 cavity configurations. 5 to 8 cavities, 20–100 ml — the highest output rate available in this machine class on ASB-12M-standard tooling.
Korea Ever-Power ISBM Series — Where HGYS150-V4-EV Fits
| Parameter | HGY150-V4 | HGYS150-V4-EV ★ | HGY200-V4-B | HGY250-V4 | HGY650-V4 |
|---|---|---|---|---|---|
| Inj. Clamp | 150 KN | 150 KN | 300 KN | 300 KN | 400 KN |
| Shot (ø50) | 310 g | 392 g ▲ | 442 g | 420 g | 480 g |
| Screw Speed | 150–270 rpm | 350 rpm ▲ | 150–270 rpm | 150–180 rpm | 150–180 rpm |
| Drive | 3 servo pumps | Full servo ▲ | 3 servo pumps | 3 servo pumps | 3 servo pumps |
| Total Power | 53.2 KW | 112.8 KW | 64.2 KW | 82.7 KW | 90.7 KW |
| Ref. Model | ASB-12M | ASB-12M full-servo | AOKI SBIII-250LL | ASB-70DPH | ASB-650 |
Frequently Asked Questions
Q1: Can my existing NISSEI ASB-12M mould tooling be used directly on the HGYS150-V4-EV?
Yes — the platen geometry matches the ASB-12M mounting standard. Submit mould drawings or photographs for a written compatibility review within 5 working days at no charge. Minor adapter plates for older mould generations are supplied at no additional cost where required.
Q2: What does <0.3% shot-weight repeatability mean in practice on a pharmaceutical line?
On a 15 g preform at 4 cavities, <0.3% variation means individual preform weights differ by less than 0.045 g per cycle across all cavity positions. This directly controls wall-thickness at the dropper neck — the parameter that determines closure torque and liner seal compliance on pharmaceutical filling lines. Pump-servo machines typically run 0.8–1.5% variation on thin-wall formats; the difference is visible as cavity-to-cavity reject rate variation.
Q3: When should I choose HGYS150-V4-EV over the standard HGY150-V4?
Choose HGYS150-V4-EV when: (1) wall-thickness tolerance requires full servo closed-loop precision — pharmaceutical droppers, thin-wall luxury cosmetic serum bottles; (2) the preform weight approaches or exceeds 310 g — the 392 g ceiling gives headroom the HGY150-V4 does not have; (3) maximum cycle speed from an existing ASB-12M mould set is the priority. Choose HGY150-V4 when pump-servo precision is sufficient and a lower capital cost is the deciding factor.
Q4: What is the actual output improvement versus HGY150-V4 on the same mould?
At ø50 mm, 350 rpm versus 180 rpm nearly doubles plasticising speed — directly shortening the injection phase per cycle. Full servo also eliminates the hydraulic pressure build-up and release delay at the start and end of each injection event. Combined, these reduce total cycle time and lift bottles per shift on the same mould and cavity count. Korea Ever-Power can model projected output improvement for your specific bottle specification and preform weight on request.
Q5: What materials does HGYS150-V4-EV process?
Standard configuration covers PET and PETG, including rPET with IV values of 0.72–0.84 dl/g. The nano far-infrared heated barrel maintains barrel temperature uniformity that is particularly beneficial for PETG optical clarity and mechanical consistency at sustained production rates. For PP, PC, Tritan, or PPSU, contact Korea Ever-Power with the specific resin datasheet.
Q6: What is the delivery lead time?
45–75 working days from order confirmation and deposit. Full-servo HGYS models typically run 10–15 days toward the longer end of that window due to servo motor integration and system calibration requirements. A production milestone schedule is issued with every order confirmation.
Q7: What spare parts availability looks like after purchase?
5-year availability commitment for consumable and wear parts. Parker valves, NSK lead screws, Yaskawa / WEICHI and Inovance servo components are stocked by regional distributors in Korea, Southeast Asia, and most ISBM markets — same-day or next-day in most cases. A recommended spare parts kit ships with each machine.
Q8: Is on-site commissioning and operator training included?
Yes, for Korea and SEA customers. A Korea Ever-Power engineer installs the machine, mounts the mould tooling, runs first-production samples to specification on-site, and completes operator training covering servo parameter setup, daily maintenance, process optimisation, and fault diagnosis — all before departure.
Q9: What warranty applies to the HGYS150-V4-EV?
12-month parts warranty from commissioning sign-off. Structural components — frame, platen, tie bars — carry a 3-year warranty. Remote diagnostic support via video call within 4 business hours; engineer dispatch within 5 business days for hardware faults not resolvable remotely.
Q10: What certifications does HGYS150-V4-EV carry?
CE marking and ISO 9001:2015 are standard on all HGYS150-V4-EV machines. CE Declaration of Conformity is available for review before order confirmation. Machine data sheet and factory acceptance test report on buyer-specified resin and cavity format are supplied at delivery.
Evaluate HGYS150-V4-EV for Your ASB-12M Line
Send Korea Ever-Power your ASB-12M mould drawings, bottle spec, target wall-thickness tolerance, and required annual output. Written mould compatibility review and projected cycle-time estimate returned within 2 business days — at no charge.
Additional information
| Editor | Cxm |
|---|
Related products
-
HGY250-V4-B ISBM Machine — Alternative to NISSEI ASB-70DPW
-
HGYS350-V4-EV Full-Servo ISBM Machine — Alternative to AOKI AL-350LL
-
HGY200-V3 ISBM Machine — Alternative to AOKI SBIII-250LL (3-Station)
-
HGY150-V3-B ISBM Machine — Alternative to AOKI SBIII-100L (3-Station)
-
HGY150-V4-B ISBM Machine — Alternative to AOKI SBIII-100L
-
HGY250-V4 ISBM Machine — Alternative to NISSEI ASB-70DPH
-
HGY200-V4-B ISBM Machine — Alternative to AOKI SBIII-250LL-50S
-
HGY150-V4 ISBM Machine — Alternative to NISSEI ASB-12M


